Industrial RO Water Treatment Plant
- Home
- »
- Turnkey Projects
- »
- RO Plant
What Is an RO Water Treatment Plant?
As water shortages and pollution increase, reverse osmosis (RO) plants have become essential for supplying clean, safe water to industries, commercial buildings and municipal users. An RO Water Treatment Plant uses membrane technology to remove dissolved salts, heavy metals, bacteria and chemical impurities. Distington Engineers & Consultants manufactures industrial RO plants designed for reliable, long-term water security.
A well-planned RO plant delivers consistent water quality, protects downstream equipment and supports sustainable water management.
How Does an RO Water Treatment Plant Work?
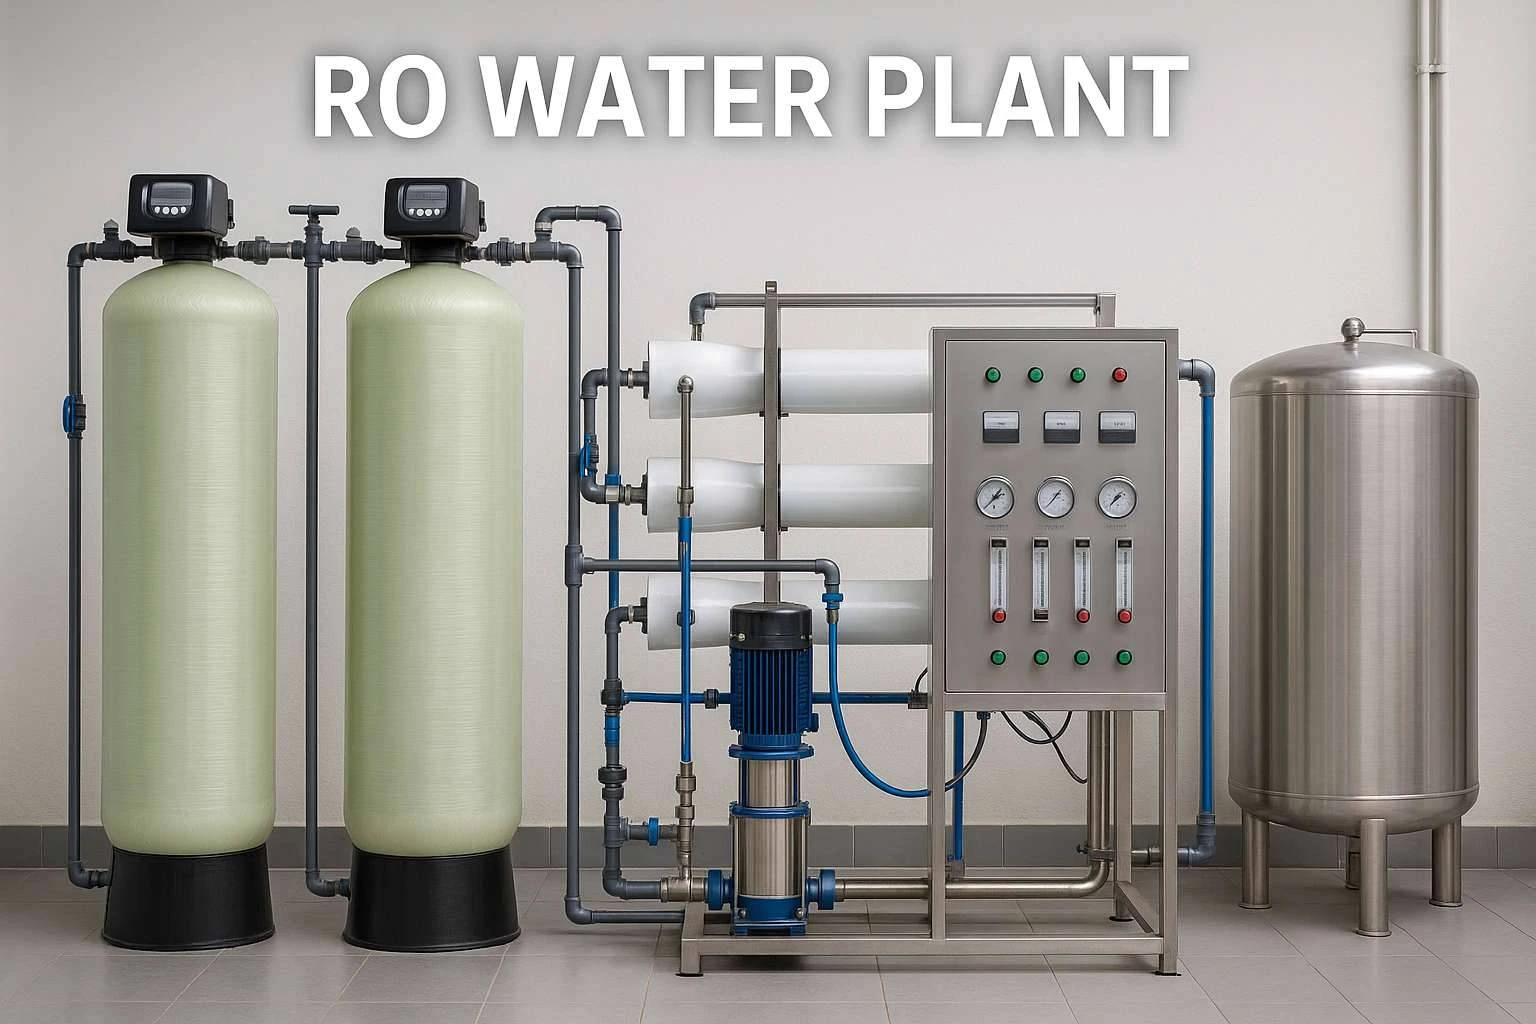
The principle on which an RO plant operates is reverse osmosis, where pressure is put on the water to push it through a semi-permeable membrane. This membrane permits the passage of water molecules but does not permit dissolved salts, minerals, bacteria, and organic contaminants to pass through.
Pre-treatment comes first. Sand filters, Activated Carbon Filters and cartridge filters remove suspended solids, chlorine and turbidity. A high-pressure pump then sends the pre-treated water through the RO membranes. Clean permeate is collected for use, while the concentrated reject stream containing the rejected impurities is discharged or recycled.
This multi-stage process delivers high-quality water for industrial and sensitive applications.
RO Plant Types and Technology
BWRO (Brackish Water RO
for borewell, municipal and other lower-TDS feed water, the most common choice for industrial process water.
SWRO (Seawater RO)
for high-TDS feed such as seawater, operating at higher pressure.
UF + RO
Ultrafiltration used as pre-treatment removes bacteria, viruses, and suspended solids, protecting the RO membranes.
Membranes are typically thin-film composite spiral-wound elements, selected according to feed water quality.
Benefits of Our Industrial RO Plant
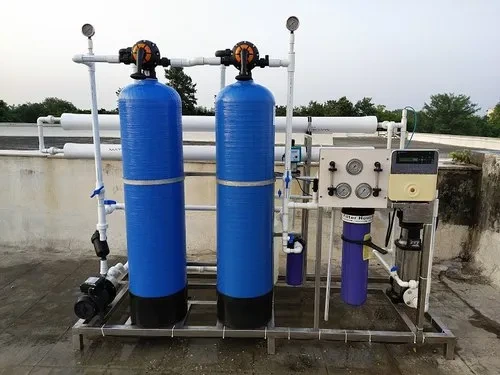
Distington industrial RO plants are designed in a way to provide excellent performance and operational efficiency.
- Consistent supply of high-purity water
- Removal of dissolved salts, heavy metals and microorganisms
- Protection of boilers, heat exchangers and process equipment
- Reduced scaling, corrosion and fouling
- Better product quality in industrial processes
- Lower operating cost through optimised recovery
These advantages render RO systems to be essential to contemporary industries.
Industrial RO Plant Specifications
| Parameter | Details |
|---|---|
| Capacity | 250 LPH – 100000 LPH |
| Plant Type | Industrial & Commercial |
| Automation | Manual / Semi Automatic / PLC |
| Membrane | As per Water Quality |
| Frame | MS / SS304 / SS316 |
| Application | Process Water, Boiler Feed, Drinking Water |
Industrial RO Plant Capacities We Manufacture
We offer Industrial RO Plants in various capacities, tailored to your water source, TDS level, and daily production needs.
Available RO Plant Capacities
- 250 LPH RO Plant – Ideal for laboratories, clinics, and small commercial applications.
- 500 LPH RO Plant – Suitable for restaurants, institutions, and small manufacturing units.
- 1000 LPH RO Plant – Designed for medium-scale industrial and commercial water treatment.
- 2000 LPH RO Plant – Reliable solution for food processing, pharmaceuticals, and manufacturing facilities.
- 5000 LPH RO Plant – High-performance system for large industrial process water requirements.
- 10,000 LPH RO Plant – Engineered for continuous industrial operations with higher water demand.
- 20,000 LPH RO Plant – Ideal for large-scale industries requiring consistent, high-quality purified water.
- Above 50,000 LPH – Fully customized industrial RO water treatment plants designed for high-capacity applications.
Projects and Case Studies
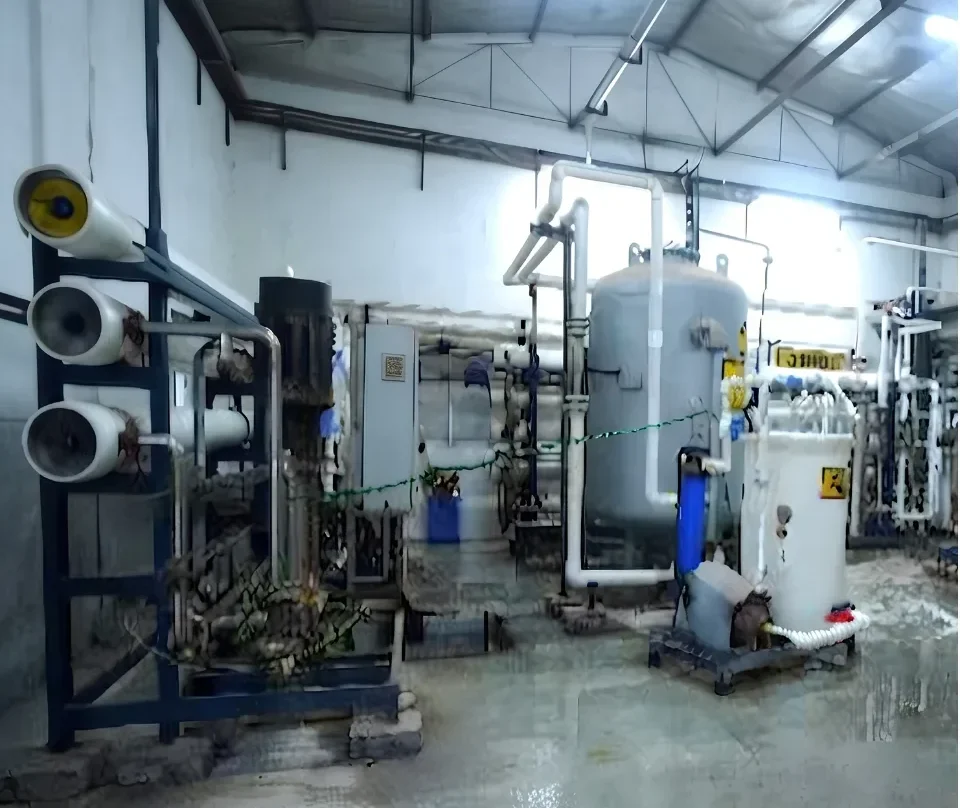
UF-RO System- 200 KLD
Reverse Osmosis (RO) & Ultra Filtration (UF) Systems
RO Plants: Remove dissolved salts, ions, and impurities for high-purity water.
UF Systems: Eliminate bacteria, viruses, and suspended solids; ideal as RO pre-treatment.
Flow Range: 250 LPH to 100 m³/h
Applications:
- Drinking Water
- Pharma
- Hotels & Resorts
- Aquaculture
- Industrial Process Water
Key Benefits:
- Energy-efficient design
- Long membrane life with advanced protection
- Fully automated or manual options
Key Features of Industrial RO Plants
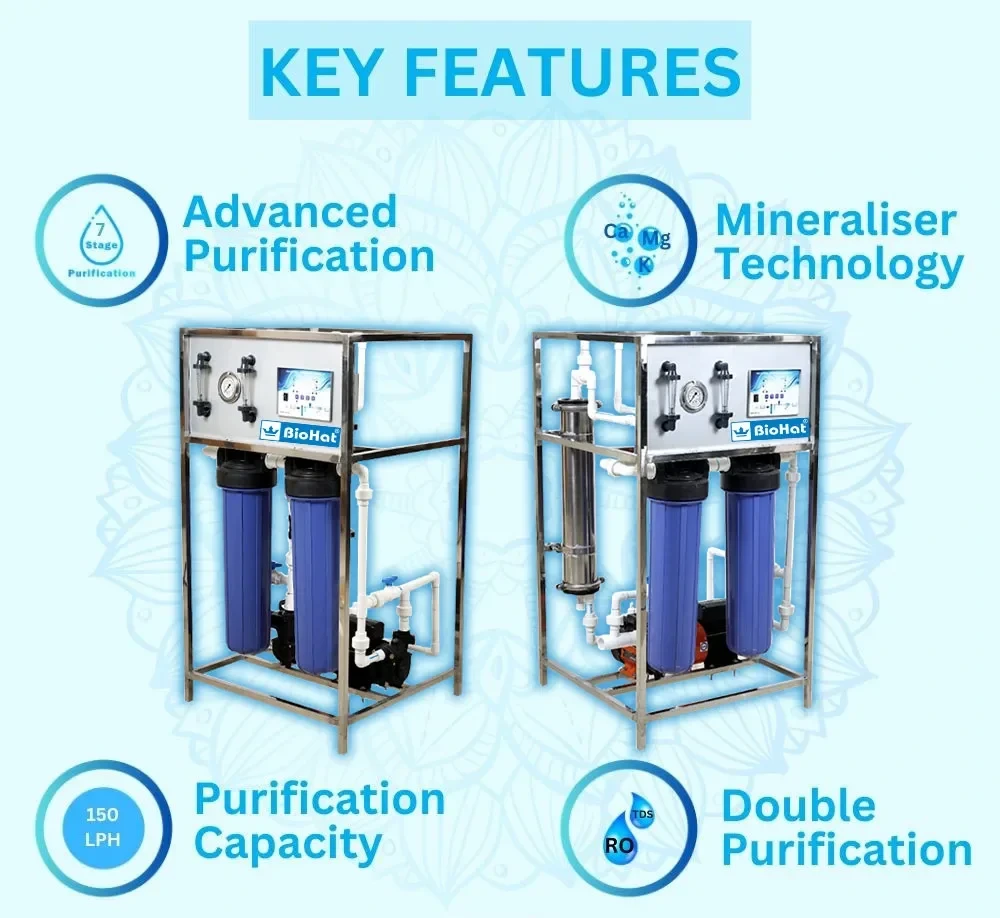
Contemporary RO plant materials are advanced and automated to be operated at a constant level. Important features include:
- High-rejection RO membranes for high-quality permeate
- Energy-efficient high-pressure pumps
- Safety-interlocked automatic control panels
- Compact, skid-mounted design for easy installation
- Online monitoring of flow, pressure and conductivity
- Chemical dosing and CIP (cleaning-in-place) systems
Distington, a leading RO Plant Manufacturer, incorporates tough materials and quality technology that will see the membranes last longer and have minimal downtime.
Applications of RO Water Treatment Plants
The application of RO water treatment plants is common in:
- The consumption of water and bottled water plants.
- Healthcare and pharmaceutical companies.
- Boiler feed water systems and power plants.
- Food and beverage processing departments.
- Electronics and semiconductor production.
- Clothing and dyeing sector.
- Hotel, hospitals, and commercial complexes.
Food & Beverage Industry-RO plants provide high-quality purified water for food processing, beverage production, and hygiene-critical operations.
They can also find application as pre-treatment to demineralization systems as well as ultrapure water generation.
Industrial RO Plant Manufacturer and Supplier in India
Distington Engineers & Consultants Pvt. Ltd. is an industrial RO plant manufacturer and supplier in India, offering RO water treatment plants from 250 LPH to 1,00,000 LPH for process water, boiler feed, pharma, food and beverage, hospitality and drinking-water applications.
Our RO systems are designed to meet your daily water needs while keeping operating cost, manpower and downtime low. Every plant includes flushing and CIP (cleaning-in-place) cycles to reduce membrane fouling and extend membrane life. After commissioning, we train your operators for smooth day-to-day running.
Distington Engineers supplies customized Industrial RO Plants across India for pharmaceutical, food processing, chemical, textile, power, hospitality, and manufacturing industries. From engineering and manufacturing to installation and commissioning, we deliver complete RO water treatment solutions designed for reliable long-term performance and efficient plant operation.
Why Choose Distington for Your RO Plant
Distington Engineers and Consultants is the provider of engineering excellence and reliable service:
Industrial and commercial designs of RO plants.
High quality of membranes and corrosion-resistant parts.
Meetings of BIS, WHO, and industrial water standards.
Professional commissioning and fast installation.
Good after-sales service and AMC support.
Low operating and maintenance cost systems.
Being a major manufacturer of RO Plants and a solution provider, Distington makes sure that the modern industries have clean, safe, and sustainable water treatment.
The selection of the appropriate RO water treatment plant will increase both the quality of water, equipment protection, and the efficiency of the process. Collaborate with Distington Engineers and Consultants to develop the future readiness RO solutions that are advanced and reliable to your operational requirements.
Why Distington Is a Trusted Industrial RO Plant Manufacturer
ISO
Certified Company
PAN MP
Service Coverage
Industrial RO Plant Manufacturer and Supplier You Can Rely On
Choosing the right Industrial RO Plant Manufacturer is critical for businesses that depend on consistent, high-purity water for daily operations. Distington Engineers and Consultants has built its reputation as a trusted Industrial RO Plant Manufacturer by delivering systems that are engineered for durability, low maintenance, and long-term efficiency across pharmaceuticals, food processing, textiles, power, and manufacturing industries.
As a complete Industrial RO Plant Supplier, we handle every stage of the project — from initial water analysis and system design to fabrication, installation, and after-sales support. Our team studies raw water quality, TDS levels, and daily production requirements before recommending a plant, ensuring you get a system that is neither undersized nor unnecessarily expensive.
Being an experienced Industrial RO Plant Manufacturer and Supplier, we understand that every industry has unique water treatment challenges. That’s why our RO plants are available in capacities ranging from 250 LPH to over 1,00,000 LPH, with automation options suited to both small commercial setups and large industrial facilities.
What sets us apart as an Industrial RO Plant Supplier:
- Pan-India supply and installation network
- Customized system design based on feed water quality and application
- High-rejection membranes with extended service life
- Transparent pricing with no hidden costs
- Dedicated technical support and AMC services post-installation
Whether you are setting up a new manufacturing unit or upgrading an existing water treatment system, partnering with an experienced Industrial RO Plant Manufacturer like Distington ensures your operations get reliable, contaminant-free water without unexpected downtime.
Frequently Asked Questions About Industrial RO Plant
An Industrial Reverse Osmosis (RO) Plant is a water purification system that uses semi-permeable membranes to remove dissolved salts, minerals, chemicals, and other impurities from water. It produces high-quality water for industrial processes, helping improve equipment performance, reduce scaling, and ensure a consistent supply of treated water for various applications.
An RO Water Treatment Plant works by forcing water through a semi-permeable membrane under high pressure. Before reaching the membrane, the water passes through pre-treatment filters to remove suspended solids, chlorine, and other impurities. The RO membrane then removes dissolved salts, minerals, and contaminants, producing high-quality purified water for industrial and commercial applications.
Industrial RO Plants are widely used in industries that require high-quality purified water. Common sectors include pharmaceuticals, food and beverage, power plants, chemicals, textiles, electronics, automotive, paper and pulp, steel, and manufacturing. These systems help improve process efficiency, protect equipment, and ensure a consistent supply of treated water.
Distington Engineers & Consultants is an Industrial RO Plant manufacturer and supplier based in Indore, India, providing customized reverse osmosis systems from 250 LPH to over 1,00,000 LPH for pharmaceutical, food processing, textile, power and manufacturing industries, with installation, commissioning and AMC support across India.
We manufacture Industrial RO Plants in a wide range of capacities to meet diverse industrial and commercial water treatment requirements. The plant capacity is customized based on factors such as daily water demand, feed water quality, and application. We can design and supply RO systems tailored to your specific project requirements.
Yes, we design and manufacture customized Industrial RO Plants based on your water quality, required treatment capacity, application, and operational requirements. Our solutions are engineered to deliver reliable performance, efficient water purification, and long-term operational efficiency for a wide range of industries.
Yes, we provide installation and commissioning services for Industrial RO Plants across India. Our experienced team handles system installation, testing, commissioning, and operator training to ensure reliable performance and efficient operation from day one.
An RO (Reverse Osmosis) Plant uses membrane filtration specifically to remove dissolved salts and impurities from water, while a Water Treatment Plant (WTP) is a broader system that may include filtration, softening, clarification and other processes — RO is often one stage within a larger WTP
Choosing the right Industrial RO Plant depends on factors such as feed water quality, required water output, daily capacity, recovery rate, application, available space, and operating costs. A professional water analysis and technical assessment help determine the most suitable RO system for your specific industrial requirements, ensuring reliable performance and cost-effective operation.
Regular maintenance is essential to ensure the efficient performance and long service life of an RO plant. It includes periodic filter replacement, membrane cleaning, system inspection, pump and valve checks, water quality monitoring, and preventive maintenance. Proper maintenance helps improve efficiency, reduce downtime, and extend the lifespan of the system.
Need a Customized Industrial RO Plant?
Share your water quality, required capacity, and application details. Our experts will recommend the most suitable Industrial RO Water Treatment Plant for your business.